


毛刺去不干净,压力调再高也没用
作者:创始人来源:https://www.jnthcsb.com/时间:2026-10-12
CNC加工中心下来的零件,边角上总带着大小不一的毛刺。手工去毛刺效率低、一致性差,用高压水射流去毛刺是更出色的选择。但很多工厂上了CNC高压清洗机之后发现,毛刺还是去不干净,尤其交叉孔和深孔里的毛刺,水冲了半天纹丝不动。问题不在压力不够,在射流有没有打到毛刺上。
The parts produced by CNC machining centers always have burrs of varying sizes on their edges and corners. Manual deburring has low efficiency and poor consistency, using high-pressure water jet to deburr is a more efficient choice. But many factories have found that after installing CNC high-pressure cleaning machines, burrs still cannot be removed completely, especially in cross holes and deep holes, which have been washed with water for a long time without any improvement. The problem is not insufficient pressure, but whether the jet hits the burrs.
毛刺的位置,决定了喷嘴怎么布局。
The location of the burrs determines how the nozzle is arranged.
CNC加工产生的毛刺,位置和加工路径直接相关。铣削的毛刺在刀具出口处,钻削的毛刺在孔的两端,交叉孔的毛刺藏在内壁交汇处。不同位置的毛刺,需要不同角度的射流去冲击。如果喷嘴只从固定方向喷射,交叉孔内部的毛刺可能被孔壁挡住,水流进不去。去毛刺效果好的设备,喷嘴布局是根据零件的具体特征设计的——哪里是加工面、哪里是交叉孔、毛刺集中在哪个区域,都要提前分析清楚。
The burrs generated by CNC machining are directly related to their location and machining path. The burrs from milling are located at the tool exit, the burrs from drilling are located at both ends of the hole, and the burrs from intersecting holes are hidden at the intersection of the inner wall. Burrs at different positions require jets from different angles to impact. If the nozzle only sprays from a fixed direction, the burrs inside the cross hole may be blocked by the hole wall, preventing water from flowing in. The nozzle layout of equipment with good deburring effect is designed based on the specific characteristics of the parts - where is the machining surface, where is the cross hole, and where the burrs are concentrated, all need to be analyzed in advance.
压力不是越高越好,要看毛刺的根部厚度。
The higher the pressure, the better. It depends on the thickness of the burr at the root.
毛刺有大有小。薄片状的毛刺,中等压力就能冲掉;根部厚实的毛刺,需要更高的冲击力。但压力太高,可能损伤零件的加工面——铝合金零件表面被高压水打出凹坑,精度就毁了。行业经验是:精加工零件用中低压大流量,粗加工零件可以适当提高压力。喷嘴的孔径和喷射距离也要匹配,孔径小压力集中但覆盖面积小,孔径大覆盖广但冲击力分散。
Burrs come in various sizes. Thin burrs can be washed away with moderate pressure; Thick burrs at the root require higher impact force. But if the pressure is too high, it may damage the machining surface of the parts - the surface of the aluminum alloy parts will be pitted by high-pressure water, and the accuracy will be destroyed. Industry experience is that for precision machined parts, medium and low pressure with high flow rates are used, while for rough machined parts, the pressure can be appropriately increased. The aperture and spraying distance of the nozzle should also be matched. A small aperture concentrates pressure but covers a small area, while a large aperture covers a wide area but disperses the impact force.
多轴旋转喷淋,是解决复杂零件的思路。
Multi axis rotating spray is the approach to solving complex parts.
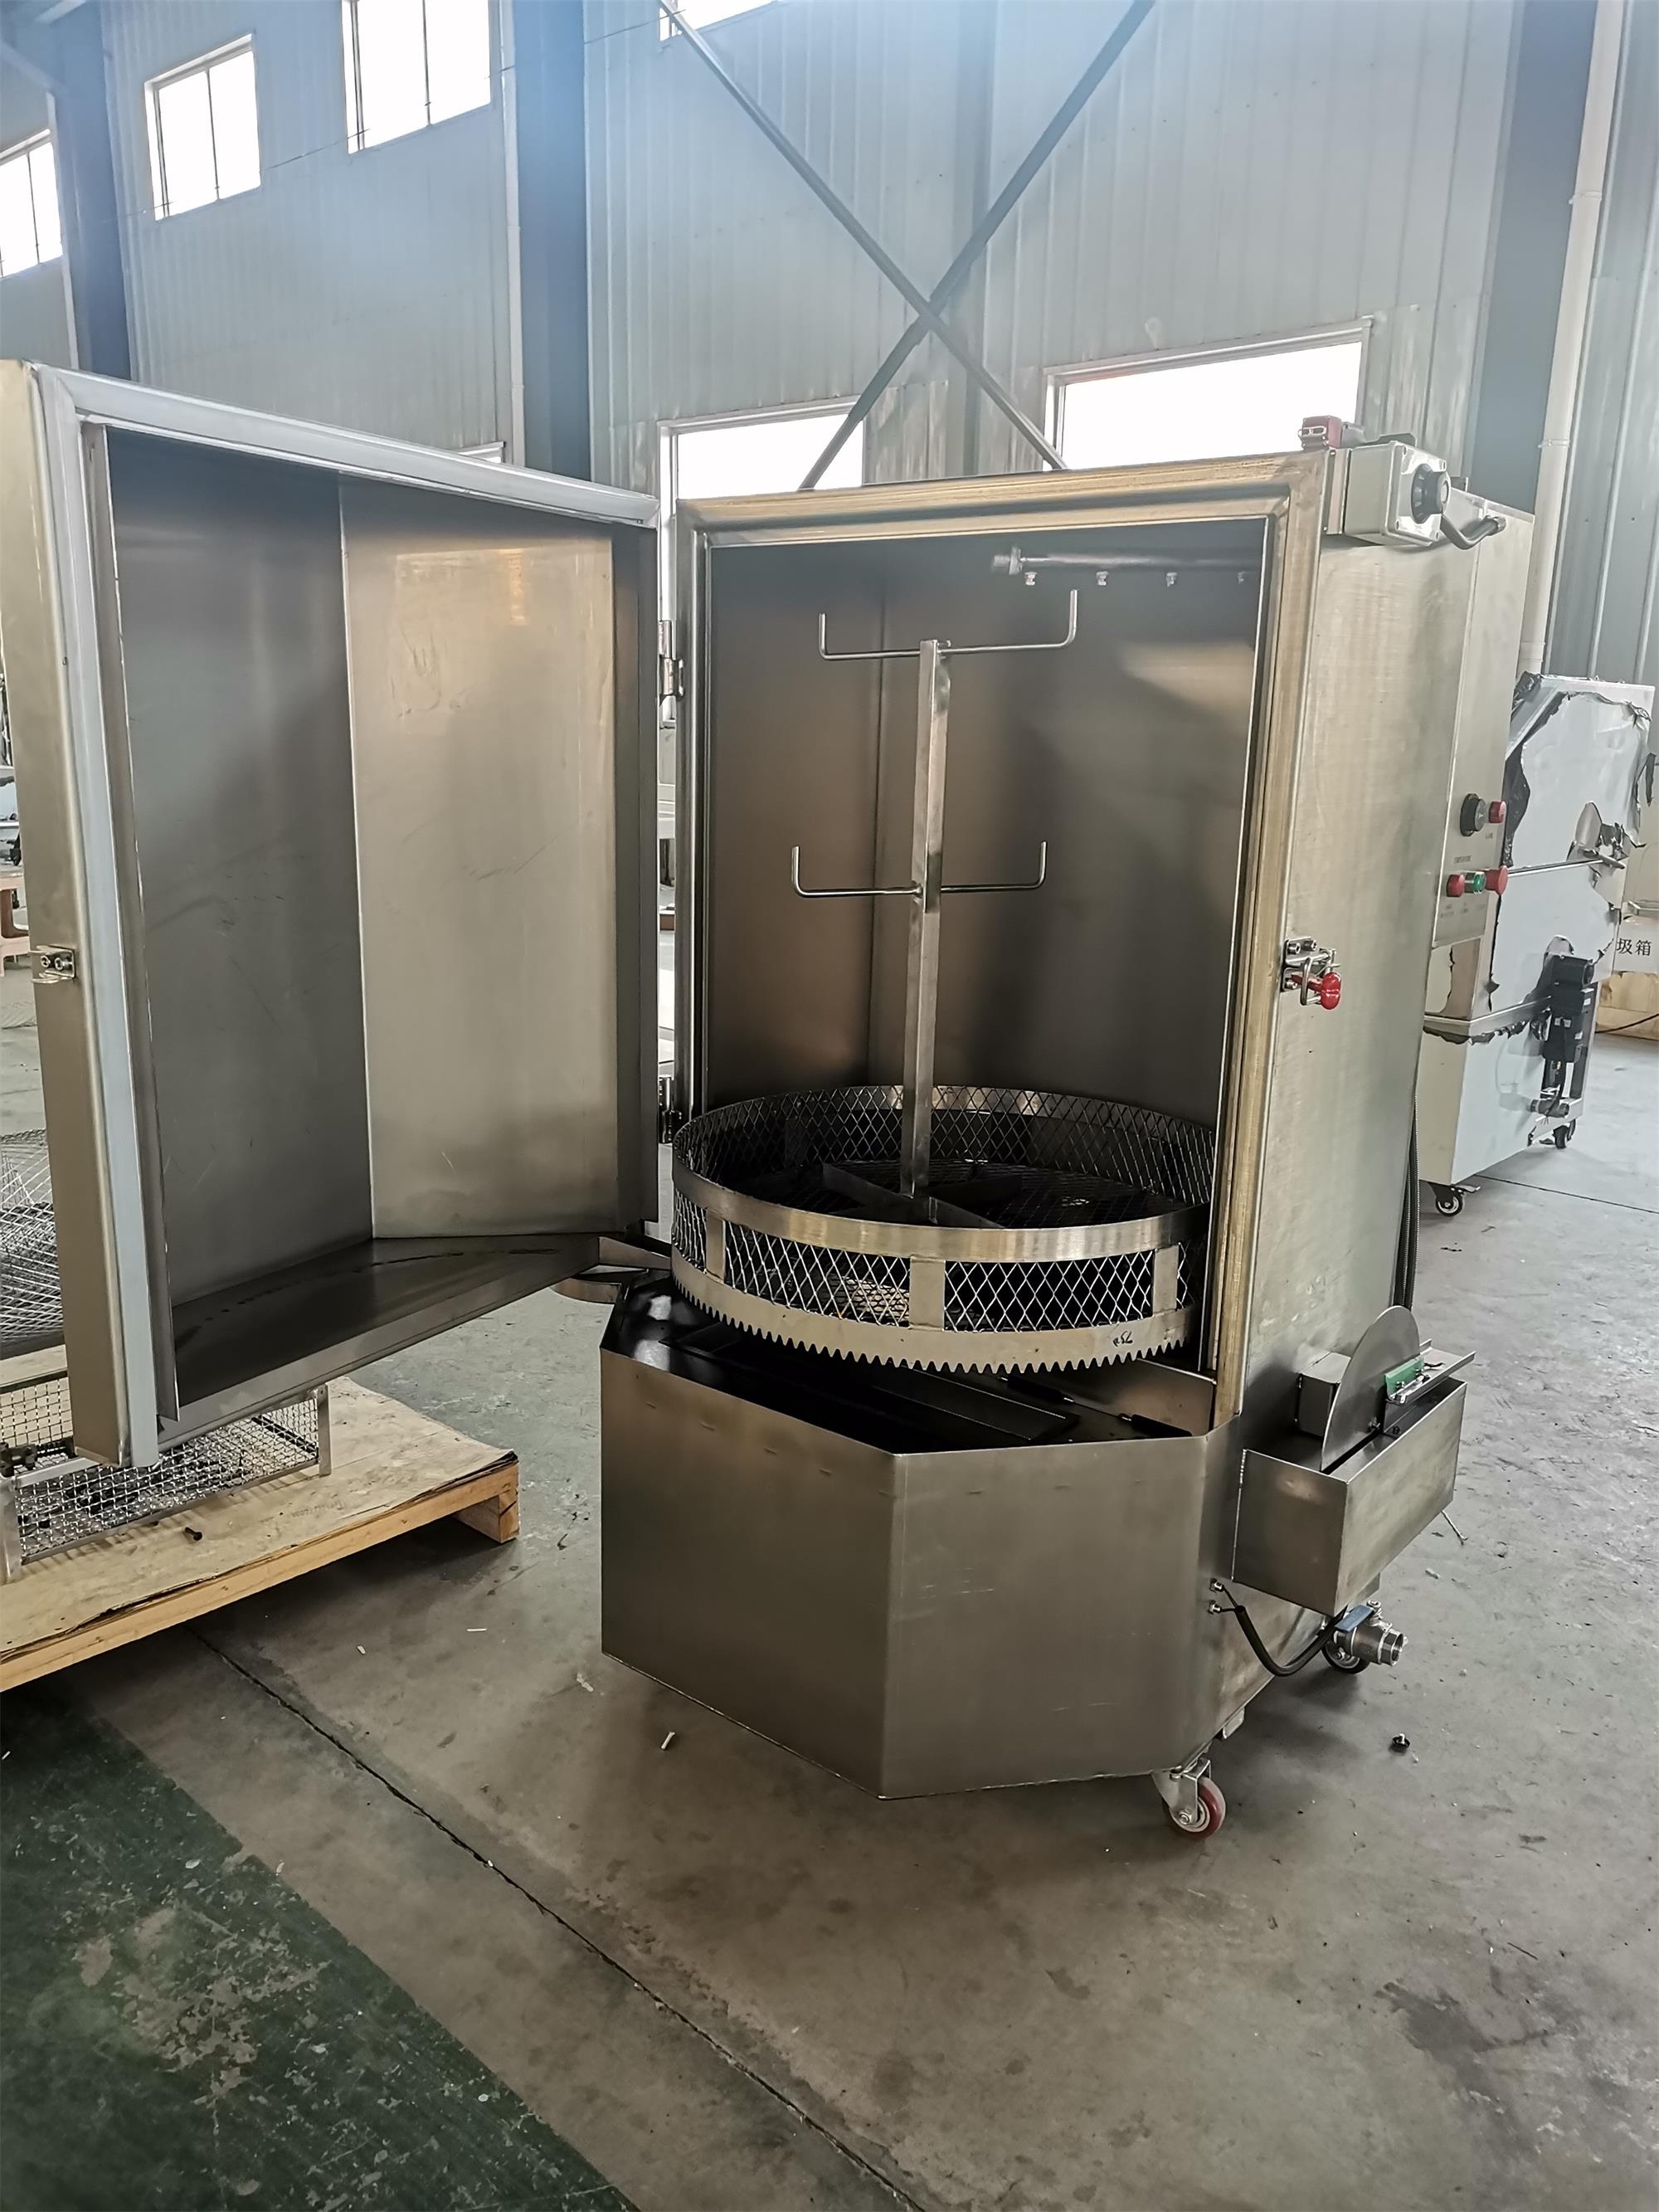
对于形状复杂、毛刺分布在不同方向的零件,固定喷嘴很难全覆盖。多轴旋转喷淋的方案是让工件在清洗过程中旋转,或者让喷淋臂围绕工件运动,使射流能从不同角度冲击毛刺。单工位旋转喷淋设备就是针对这类需求设计的——工件装夹后旋转,喷嘴从多个方向喷射,交叉孔和深孔大多能照顾到。
For parts with complex shapes and burrs distributed in different directions, it is difficult to fully cover them with a fixed nozzle. The solution of multi axis rotating spray is to rotate the workpiece during the cleaning process, or to move the spray arm around the workpiece, so that the jet can impact the burrs from different angles. The single station rotary spray equipment is designed for this type of requirement - the workpiece is clamped and rotated, and the nozzle sprays from multiple directions, accommodating both cross holes and deep holes.
水温对去毛刺效果有影响,容易被忽略。
The water temperature has an impact on the deburring effect and is easily overlooked.
高压水射流去毛刺,水温高一些效果更好。热水能软化毛刺根部的材料,降低毛刺的强度,同时水的粘度降低,射流更集中。通常水温控制在50-70℃之间。但水温高了,设备的密封件和管路要能耐受,不是所有高压清洗机都支持热水运行。
High pressure water jet deburring is more effective at higher water temperatures. Hot water can soften the material at the root of burrs, reduce the strength of burrs, and at the same time, lower the viscosity of water, making the jet more concentrated. Usually, the water temperature is controlled between 50-70 ℃. But when the water temperature is high, the sealing components and pipelines of the equipment should be able to withstand it. Not all high-pressure cleaning machines support hot water operation.
过滤系统决定设备能不能连续稳定运行。
The filtering system determines whether the equipment can operate continuously and stably.
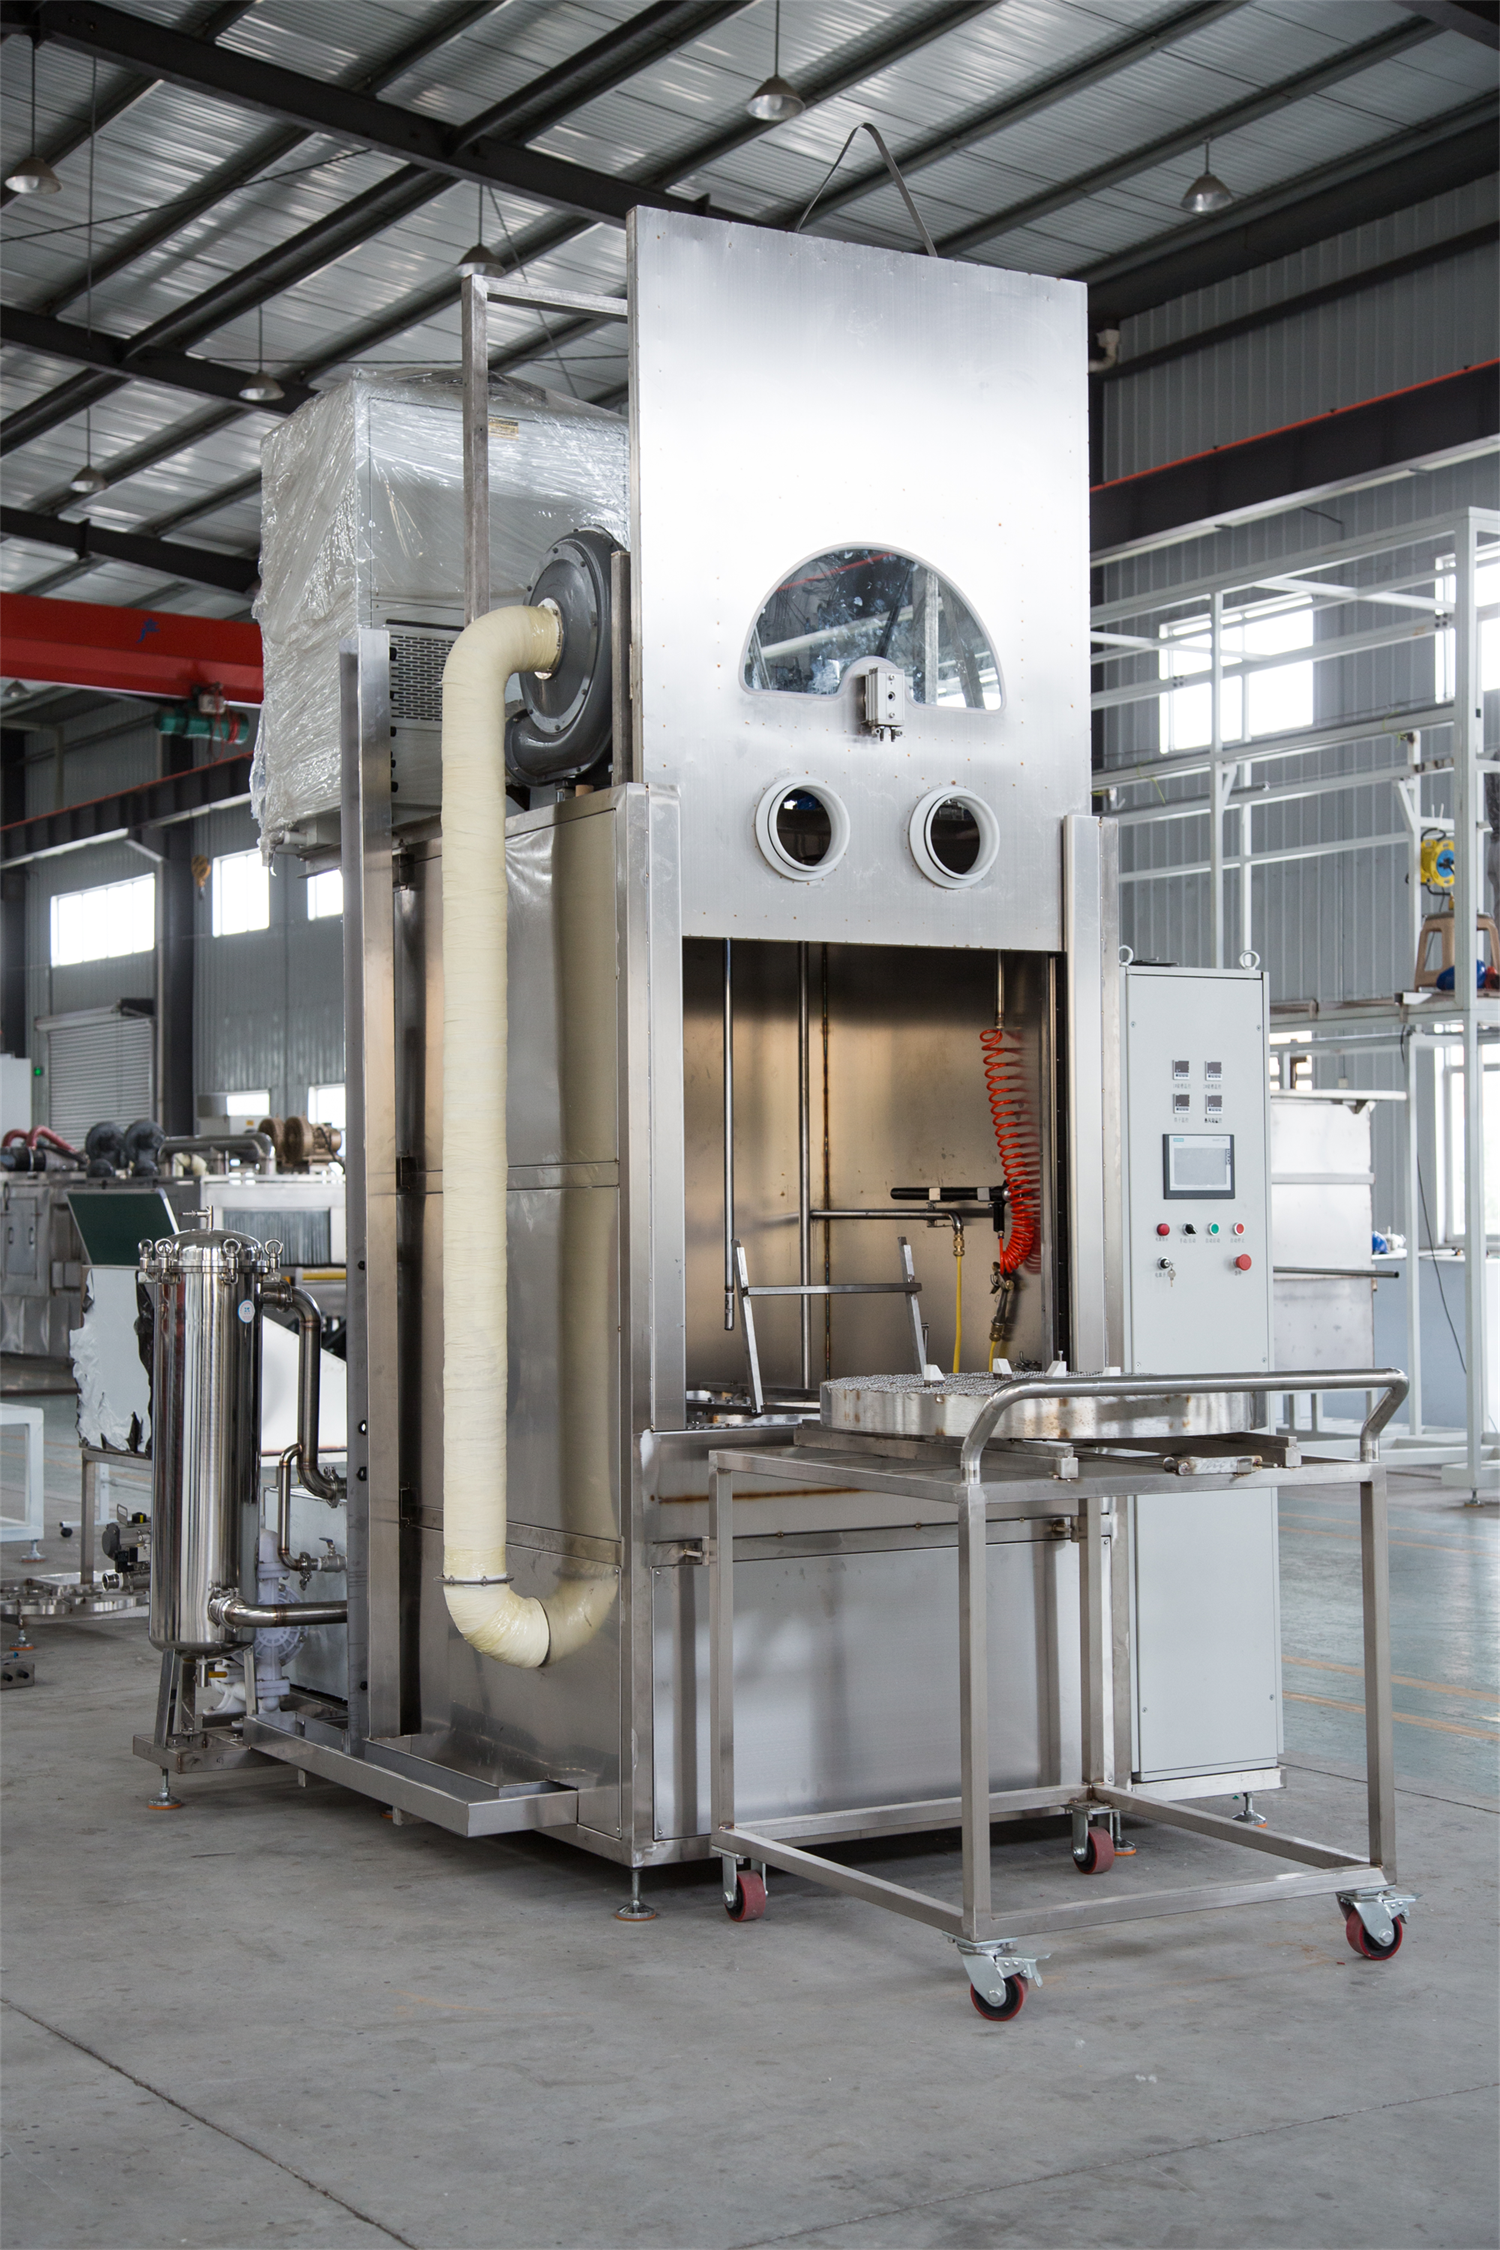
去毛刺过程中冲下来的金属碎屑混入水箱,如果不及时过滤,会随水流再次打到零件表面,划伤加工面。更严重的是,碎屑进入高压泵,会磨损柱塞和密封件。多级过滤(粗滤、精滤、磁性过滤)配合使用,才能保证水质洁净。滤芯要按压差更换,不能等堵死了才想起来。
The metal debris washed down during the deburring process mixed into the water tank. If not filtered in time, it will hit the surface of the parts again with the water flow, scratching the machined surface. More seriously, debris entering the high-pressure pump can wear down the plunger and seals. The combination of multi-stage filtration (coarse filtration, fine filtration, magnetic filtration) is necessary to ensure clean water quality. The filter element needs to be replaced due to pressure difference, and we cannot wait until it is blocked to remember.
CNC高压清洗机的选型逻辑很清晰:先分析零件的毛刺位置和特征,再设计喷嘴布局和喷射角度;压力按毛刺厚度和零件材质匹配;复杂零件考虑多轴旋转喷淋;水温控制在50-70℃;过滤系统保证水质洁净。设备是工具,射流打到毛刺上才是目的。
The selection logic of CNC high-pressure cleaning machine is very clear: first analyze the burr position and characteristics of the parts, and then design the nozzle layout and spray angle; The pressure should be matched according to the thickness of the burrs and the material of the parts; Consider multi axis rotating spray for complex parts; Control the water temperature between 50-70 ℃; The filtration system ensures clean water quality. Equipment is a tool, and the goal is to hit the burrs with a jet.
 新闻资讯
推荐文章
 联系我们
 公司:济南科尔超声波设备有限公司
 热线:18663767799
 地址:山东省济南市济阳区创业路与启航街交叉口南40米
济南科尔超声波设备有限公司
Jinan Keer ultrasonic equipment Co., Ltd
 咨询电话:18663767799
 E-MAIL:jnkergs@163.com
 地址:山东省济南市济阳区创业路与启航街交叉口南40米
 鲁公网安备 37011202001385号
扫一扫,更多精彩